Pyrometry compliance
Instruments, thermocouples and control loops must pass calibration, system accuracy tests and temperature uniformity surveys. Well-designed control and recording make those tests easier to pass and to prove.
Industry brief
Furnace control and records that stand up to every customer audit.
What matters
Heat treaters hold tight limits on time, temperature and atmosphere. Many work for aerospace and automotive customers who audit every detail. Furnaces must run safely, pass their accuracy and uniformity tests and prove that each load was treated correctly. One bad batch can mean scrapped parts and lost approvals.
Instruments, thermocouples and control loops must pass calibration, system accuracy tests and temperature uniformity surveys. Well-designed control and recording make those tests easier to pass and to prove.
Every load needs a complete, tamper-evident record of time, temperature and atmosphere, linked to the parts and recipe used, and ready to show a customer or Nadcap auditor.
Burners, fuel trains, vacuum systems and flammable or toxic atmospheres need purge, flame and interlock protection that is designed and proven to the level your risk assessment demands.
Operators should be able to load a recipe and trust it. Controlled recipe management, clear displays and alarms on any deviation keep every cycle the same, shift after shift.
Solutions
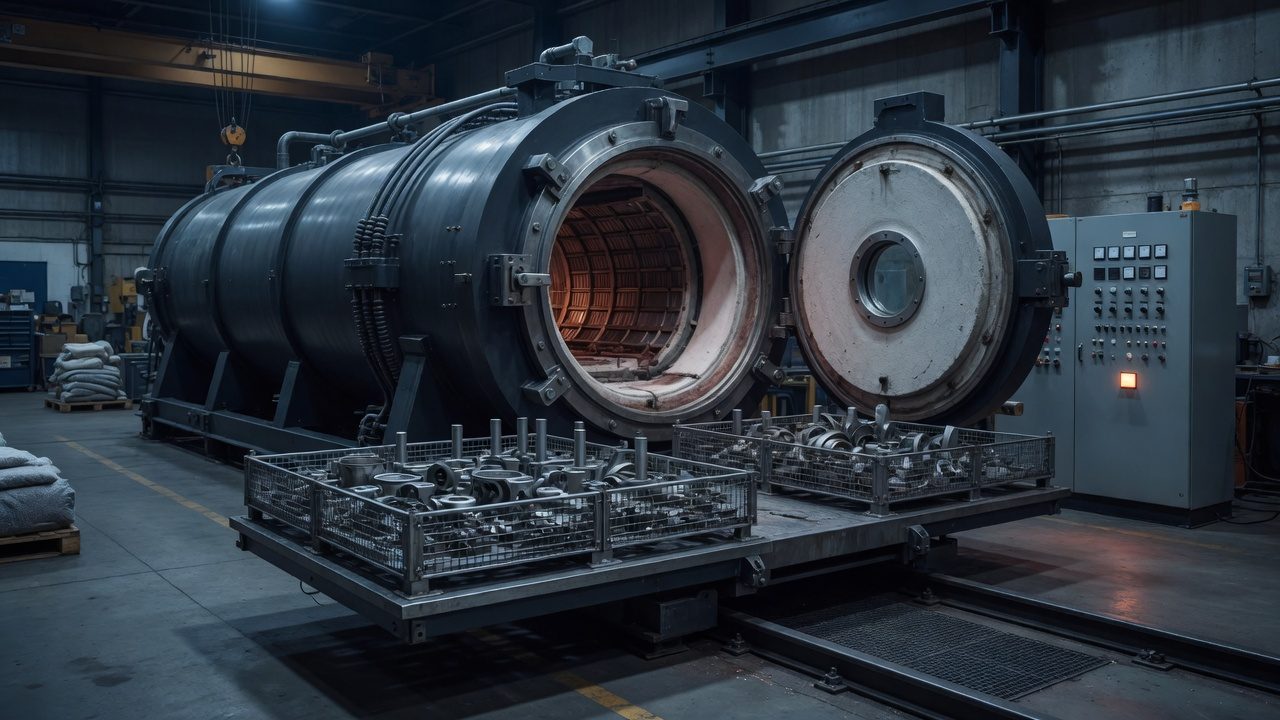
Matrix delivered the control system for a vacuum furnace. Vacuum furnaces combine pumping, heating and cooling in one tightly sequenced cycle, and their control must give repeatable results and a clear record of every load.
How we help
Furnace downtime is lost production, and changes to controls can trigger new surveys and tests. We plan upgrades around your schedule, prove recipes and logic against a simulation before site, and schedule commissioning around the tests needed to requalify each furnace. You get the design, code and documentation to run and maintain the system yourselves.
Obsolete PLCs to current platforms
In Upgrades UpgradesNew functions on a running system
In Upgrades Virtual CommissioningEquipment and process that respond
In Virtual Commissioning Virtual CommissioningEvery sequence and fault path tested
In Virtual Commissioning Code DevelopmentExisting code analysed, documented and modified
In Code Development Code DevelopmentTo the Matrix software standard
In Code DevelopmentStandards
The standards listed are those most often relevant to control-system work in this sector. Which apply to your project, and how, is agreed with you at specification stage.
| Standard | What it covers | How we work with it |
|---|---|---|
| AMS2750 | SAE aerospace pyrometry specification: sensors, instruments, calibration, accuracy tests and uniformity surveys. | Instruments, thermocouples and recording designed to meet each furnace's class and instrumentation type. |
| AIAG CQI-9 | Heat Treat System Assessment, used by automotive customers to audit heat treaters. | Process monitoring, alarms and records designed around the requirements your customers audit. |
| Nadcap heat treating (AC7102) | Audit criteria for Nadcap heat treating accreditation, required by many aerospace customers. | Recipe control and secure electronic records that support the evidence your Nadcap audit examines. |
| BS EN 746-1, BS EN ISO 13577-2 and -4 | Safety of industrial furnaces: general requirements, combustion and fuel handling, and protective systems. | Burner management, purging and furnace protective systems designed to their requirements. |
| BS EN 60204-1 | Safety of machinery: electrical equipment of machines, including stopping and emergency stop. | Control panels and machine electrics designed to it and verified before and after installation. |
| BS EN ISO 13849-1 | Design of the safety-related parts of machine control systems, rated by performance level (PL). | Safety functions designed and verified to the performance level your risk assessment requires. |
Projects
Take it with you
Contact
Standards-led, fully documented control systems that you own and can support.